Talking Pen Quality Control Checklist: Recognition, Audio, Battery, and Packaging: A talking pen quality plan should control incoming components, approved files, first-piece assembly, coded-page recognition, audio and controls, power and charging, housing workmanship, programming identity, accessories, labels, retail packaging, and shipment sampling. Each check needs a method, frequency, acceptance rule, and record.
Quality control is often reduced to a final functional test. That is too late for problems created by wrong files, drifting print conditions, mixed components, poor assembly, or incorrect pack-out. A useful plan places controls where the defect can first be detected and contained.
This guide is written for educational publishers, language-learning brands, curriculum developers, toy distributors, and sourcing teams. It addresses the questions that normally appear between the first concept discussion and a production-ready quotation: product application, customer requirements, content ownership, sample purpose, factory testing, shipment inspection, packaging, and market-specific documentation. It does not present universal specifications because talking-pen should be engineered around the final user, configuration, claims, sales market, and distribution plan.
For an overview of the available configuration and customization direction, review Cakub’s talking pens product page. Buyers who are still comparing formats can also start with the interactive learning product range.
1. What should buyers understand first?
A talking-pen control plan links a requirement to a production stage, method, equipment or reference, frequency, responsible role, acceptance rule, record, and reaction plan. It distinguishes 100% functional checks from statistical sampling and distinguishes safety-critical issues from cosmetic variation.
Practical buyer answer: Start with the approved user journey and convert every important behavior into an observable check. Then add process controls for the files, components, and assembly steps that make that behavior repeatable.
The most reliable starting point is a one-page use-case description. State who uses the product, what physical action starts the interaction, what the product should do, what happens next, and how success is observed. This prevents a supplier from substituting a familiar standard product for a requirement that actually needs different electronics, files, construction, firmware, or packaging.
2. Where does this solution fit—and where does it not?
The checklist should be adapted to the exact model, content library, printed media, battery, accessories, packaging, market, and known supplier risks.
| Decision question | Good fit when | Reconsider when |
|---|---|---|
| Is the requirement observable? | Recognition, audio, control, appearance, and pack-out criteria have examples or limits. | Terms such as good quality or normal sound are left subjective. |
| Is the stage appropriate? | Wrong components and files are detected before assembly or programming at scale. | All defects are expected to be found after packing. |
| Is the reaction defined? | Failed lots are contained, investigated, corrected, and rechecked before release. | Operators record a failure but production continues without disposition. |
3. Which specification decisions change the project?
A checklist becomes effective when each item has a reference and consequence, not simply a box to tick.
1. Critical-to-quality list
Identify safety, recognition, content identity, electrical, workmanship, labeling, and packaging characteristics that affect acceptance. This decision should be closed before detailed quotation because it affects several downstream assumptions. For talking-pen, the useful question is not whether a feature is available in theory, but how it will be implemented, approved, repeated in production, and checked before shipment.
2. Inspection stage
Place checks at incoming, first-piece, in-process, line test, final audit, and shipment inspection according to cause. A supplier can only validate this point when the intended user action and acceptable response are observable. For talking-pen, the useful question is not whether a feature is available in theory, but how it will be implemented, approved, repeated in production, and checked before shipment.
3. Test coverage
Choose 100% checks for high-risk functions and a documented sampling basis for suitable attributes. Treat this as a controlled product requirement rather than an informal preference in an email thread. For talking-pen, the useful question is not whether a feature is available in theory, but how it will be implemented, approved, repeated in production, and checked before shipment.
4. Reference set
Control the approved sample, artwork, firmware, audio manifest, coded pages, labels, accessories, packaging, and defect examples. The approved sample should demonstrate this requirement with representative content and production-style materials. For talking-pen, the useful question is not whether a feature is available in theory, but how it will be implemented, approved, repeated in production, and checked before shipment.
5. Equipment and fixtures
Specify test pages, chargers, cables, gauges, audio references, programming readers, and calibration or verification status. Document the decision in the specification, sample comments, and final inspection checklist so each team uses the same reference. For talking-pen, the useful question is not whether a feature is available in theory, but how it will be implemented, approved, repeated in production, and checked before shipment.
6. Reaction plan
Define stop, segregate, trace, investigate, correct, rework, re-test, escalate, and release authority. If the requirement is still open, ask the supplier to quote the alternatives separately instead of hiding the difference in one price. For talking-pen, the useful question is not whether a feature is available in theory, but how it will be implemented, approved, repeated in production, and checked before shipment.
| Decision area | What to define | Approval evidence |
|---|---|---|
| Critical-to-quality list | Identify safety, recognition, content identity, electrical, workmanship, labeling, and packaging characteristics that affect acceptance. | Specification, approved sample, or controlled record |
| Inspection stage | Place checks at incoming, first-piece, in-process, line test, final audit, and shipment inspection according to cause. | Specification, approved sample, or controlled record |
| Test coverage | Choose 100% checks for high-risk functions and a documented sampling basis for suitable attributes. | Specification, approved sample, or controlled record |
| Reference set | Control the approved sample, artwork, firmware, audio manifest, coded pages, labels, accessories, packaging, and defect examples. | Specification, approved sample, or controlled record |
| Equipment and fixtures | Specify test pages, chargers, cables, gauges, audio references, programming readers, and calibration or verification status. | Specification, approved sample, or controlled record |
| Reaction plan | Define stop, segregate, trace, investigate, correct, rework, re-test, escalate, and release authority. | Specification, approved sample, or controlled record |
Need a product-specific QC checklist?
Send the configuration, approved sample status, book set, market, packaging, quantity, and known risks.
4. What should the buyer prepare before requesting a quotation?
A useful quotation pack reduces assumptions without pretending every decision is final. It should distinguish confirmed requirements, preferred options, open questions, buyer-supplied files, supplier responsibilities, and items that will be approved through sampling. For talking-pen, prepare the following:
- Approved reference set: Provide signed product, coded books, firmware ID, audio manifest, artwork, accessories, labels, and packaging specification.
- Defect classification: Define critical, major, and minor examples plus special accept/reject rules for content and function.
- Inspection plan: State lot definition, sampling basis, test quantities, frequency, equipment, records, and disposition authority.
- Market and age grading: List destination countries, intended user age, sales channel, product claims, and any buyer-specific compliance manual.
- Commercial range: Provide forecast quantity, launch quantity, packaging format, delivery window, and preferred shipping basis.
- Ownership and approvals: Identify who owns artwork and audio, who approves firmware behavior, and who signs the production-intent sample.
Do not send a large folder without an index. Add a requirement sheet that lists every file, its revision, language, owner, intended use, and approval status. If the project contains many tracks, cards, pages, triggers, or modes, include a mapping table that connects the physical action to the expected response. This table becomes valuable during firmware review, factory testing, and shipment inspection.
5. How should development move from concept to shipment?
Build the control plan during engineering, verify it in pilot production, and revise it when failures reveal an uncontrolled cause.
- Confirm the requirement brief: List user-critical functions, safety characteristics, visible quality, content identity, accessories, labels, and packaging. Record open questions, the responsible party, and the required approval evidence before moving forward.
- Create the controlled map: Connect each requirement to process stage, method, fixture, frequency, limit, record, and reaction. Use controlled filenames and revision dates so artwork, audio, firmware, components, and packaging cannot drift apart.
- Review feasibility and risk: Review component, file, print, programming, assembly, and pack-out failure modes before approving the line. Review the result against the intended user journey, not only against an isolated component demonstration.
- Build a purpose-defined prototype: Run the proposed checklist during a pilot or production-intent build and improve unclear methods before mass production. Keep one approved reference and convert every comment into a measurable acceptance point.
- Approve a production-intent sample: Combine final-style reference sample, coded media, firmware, audio manifest, defect examples, labels, accessories, and packaging and close measurable comments before material release. Confirm that buyer-supplied files and factory-prepared files use the same version before releasing materials.
- Release controlled production files: Freeze the bill of materials, control plan, test instructions, defect catalogue, programming records, inspection reports, packaging artwork, test method, and approval references. Do not compress the schedule by removing a validation gate; resolve the cause of delay and re-plan the critical path.
- Inspect and release the shipment: Sample across the order, reproduce representative user journeys, verify pack-out, and document disposition before dispatch. Before shipment, reproduce representative user actions and compare the packed product with the signed approval set.
The workflow should have visible gates. A concept sample proves feasibility; an engineering sample closes construction and function; a production-intent sample confirms controlled files, materials, firmware, audio, artwork, accessories, and packaging. Combining those purposes into one vague “sample” makes approval comments hard to interpret and makes schedule promises unreliable.
6. What should factory testing and shipment inspection cover?
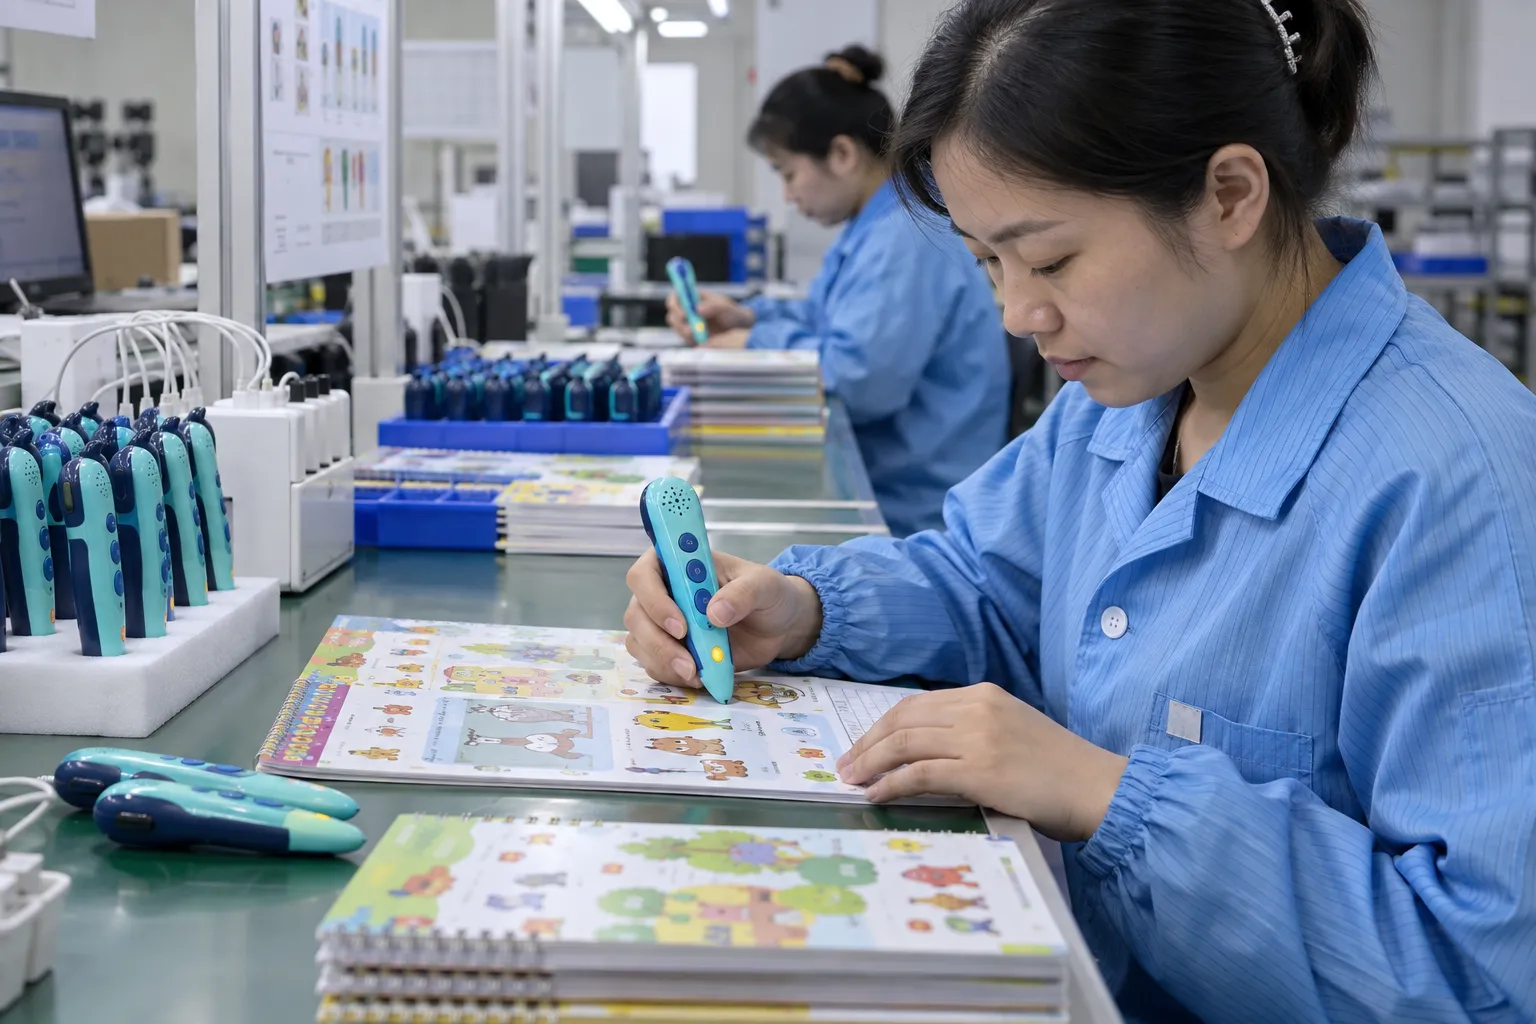
Testing should reproduce meaningful user actions while also confirming process identity and traceability.
| Control point | Practical check | Evidence |
|---|---|---|
| Incoming identity | Verify key electronic parts, battery, housing, speaker, accessories, printed media, and supplier lot records. | Record result, defect category, and sample identity |
| First-piece approval | Confirm assembled appearance, recognition, audio, controls, power, programming, and fit before full line release. | Record result, defect category, and sample identity |
| 100% line function | Use controlled test media and clear pass/fail signals for recognition, audio, buttons, charging, and programmed identity. | Record result, defect category, and sample identity |
| Pre-shipment sampling | Select across cartons and production periods; test varied content and compare complete pack-out with approvals. | Record result, defect category, and sample identity |
| Recognition consistency | Activate representative points across pages, edges, colors, and different positions in the content library. | Record result, defect category, and sample identity |
| Audio and controls | Verify track mapping, clarity, volume steps, buttons, charging behavior, and low-power response. | Record result, defect category, and sample identity |
| Print-to-device match | Compare coded production pages, controlled mapping data, firmware, and the approved pen. | Record result, defect category, and sample identity |
| Retail pack-out | Confirm accessories, instructions, labels, inserts, protective fit, barcode placement, and carton quantity. | Record result, defect category, and sample identity |
Testing frequency should be based on risk, process capability, component history, and the consequence of a failure. Some functions may justify a 100% production check, while appearance or packaging characteristics may be evaluated through a defined sampling plan. The ISO 28590 overview explains the role of acceptance sampling by attributes, but the buyer and inspection provider still need a written defect list, sampling basis, and accept/reject rules for the actual order.
Shipment inspection should use the approved product, controlled files, packing specification, label artwork, and purchase order as references. Inspectors should test content from different parts of the library rather than replaying one demonstration item. Allow time before the shipping deadline for containment, root-cause review, corrective action, and reinspection when needed.
See Cakub’s quality-control workflow for the broader sequence from incoming materials through shipment release, or review the factory capability page when evaluating production support.
7. How should safety and compliance planning be handled?
Compliance depends on intended use, age grading, materials, electronics, power source, wireless functions, sound output, accessories, packaging, claims, and destination market. Start planning before the final design because required tests, warnings, traceability marks, battery construction, or technical documentation can affect the product itself.
- U.S. CPSC toy safety guidance — use the current official text as a starting point for the final model and market.
- European Commission toy-safety information — use the current official text as a starting point for the final model and market.
- IEC 62115 electric-toy standard overview — use the current official text as a starting point for the final model and market.
Relevant official starting points for this topic include U.S. CPSC toy safety guidance, European Commission toy-safety information, IEC 62115 electric-toy standard overview. These links do not determine the complete test plan. Ask an accredited laboratory or qualified compliance adviser to review the final configuration and the markets where the product will be placed. Keep reports, declarations, bills of materials, label approvals, and production identities connected to the exact model and revision.
8. How can buyers compare supplier quotations fairly?
Quality-support quotations should state included line tests, inspection records, buyer audit support, fixtures, sample quantity, laboratory coordination, third-party inspection access, reinspection, and corrective-action responsibilities.
Normalize quotations into the same structure: product configuration, included content volume, electronic functions, materials, accessories, retail packaging, master-carton basis, development charges, sample rounds, tooling, testing, documentation, quantity, currency, Incoterm, payment assumptions, and validity period. Highlight every exclusion. Two unit prices are not comparable when one includes programmed content, printed media, accessories, or inspection support and the other does not.
9. Common mistakes that create avoidable delay or rework
Using one golden sample without files
A physical sample cannot identify which firmware, audio, code map, label, and packaging revisions created it. The practical correction is to add an owner, reference file, approval point, and inspection method before the order enters mass production.
Testing the same page repeatedly
A narrow demonstration misses library boundaries, print variation, language errors, and neighboring-zone risks. The practical correction is to add an owner, reference file, approval point, and inspection method before the order enters mass production.
Leaving cosmetic criteria subjective
Color, gaps, marks, print variation, and assembly appearance need controlled references or measurable limits. The practical correction is to add an owner, reference file, approval point, and inspection method before the order enters mass production.
Scheduling inspection on ship day
There is no practical time to contain, correct, rework, and re-inspect a failed lot. The practical correction is to add an owner, reference file, approval point, and inspection method before the order enters mass production.
10. Frequently asked questions
Should every talking pen be function tested?
High-risk core functions are often suitable for 100% line testing, but the exact plan depends on process capability and consequence. Shipment inspection still samples complete products independently.
What is AQL in talking pen inspection?
AQL-based sampling is a lot-acceptance tool for defined defect classes, not a promise that the lot contains that exact defect percentage. Agree the sampling standard, lot, levels, limits, and special tests.
How can audio mapping be inspected?
Use a controlled test list that samples different titles, pages, languages, functions, and library positions, then compare observed playback with the approved mapping database.
What battery checks are useful?
Checks may include identity, voltage or state, charging indication, current behavior, runtime sampling, low-power response, battery access, protection, and transport documentation depending on configuration.
What should happen after a failed inspection?
Contain the lot, document findings, investigate scope and root cause, define corrective action, rework when authorized, and complete an independent reinspection against the agreed plan.
Conclusion: approve a repeatable product system
Convert quality expectations into a staged, evidence-based control plan. When files, print, electronics, assembly, function, labels, and pack-out remain traceable, final inspection confirms a controlled process instead of searching for unknown problems.
A successful talking-pen project is not defined by a single attractive sample. It is defined by whether the approved user experience can be reproduced with controlled files, stable materials, clear workmanship criteria, suitable factory testing, traceable packaging, and a shipment-inspection method that reflects customer requirements. That is the standard buyers should use when comparing suppliers and deciding whether a project is ready for production.
Planning a custom talking-pen project?
Send your target user, product format, content scope, market, quantity range, packaging, and launch timing for a structured project review.